Configuring a Composite Autoclave for New Energy Battery Shell Production: An Application Guide
A composite autoclave built for battery-shell and photovoltaic-module work is specified around production rhythm first and peak pressure second. For plants running 8–16 hours a day, three decisions shape the machine: continuous multi-batch operation with automated feeding, curing and discharging; anti-leakage and over-pressure protection sized for unattended cycles; and energy consumption held to 0.5–0.7 kWh per cubic meter of chamber volume. Supporting equipment, plant conditions and export certification complete the package.
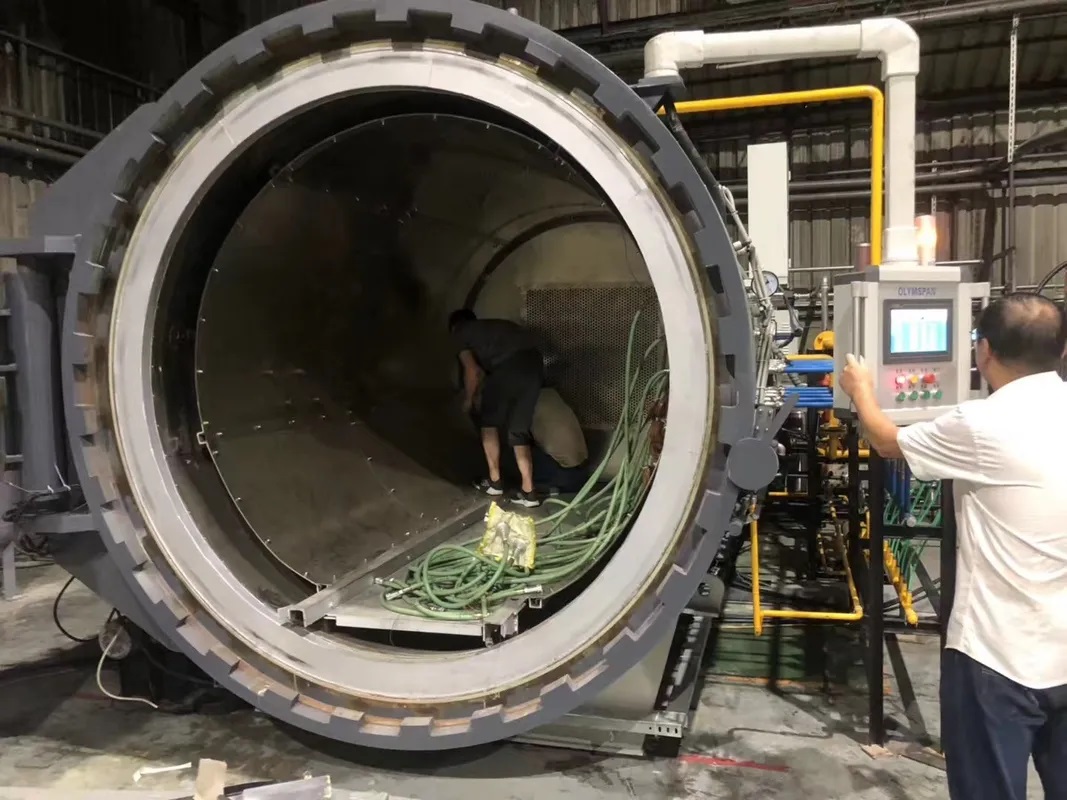
A composite autoclave is a heated pressure vessel that cures a laminate under combined temperature, pressure and vacuum. In new energy production it consolidates battery-shell and photovoltaic-module laminates to a controlled thickness, drives out internal voids, and repeats the same cycle across many batches per day.
Olymspan (Jiangsu Olymspan Equipment Technology Co., Ltd.) is a manufacturer based in Henglin town, Changzhou city, Jiangsu province, China, established in 2004 as a subcompany of the WULIN group. The company designs and manufactures industrial autoclaves and lists composite autoclaves, carbon fiber products, carbon fiber drones and tube heat exchangers among its main products.
The Configuration Brief in One Page
A new energy battery-shell line does not need the highest pressure envelope available on the market. It needs a machine whose duty cycle, safety logic and running cost match a factory floor that runs daytime shifts with a light dust load and a standard 380 V supply. The configuration brief therefore reduces to seven requirement groups.
- Duty cycle: continuous multi-batch operation, 8–16 hours per day, with automatic feeding, curing and discharging sequences.
- Flexibility: the ability to cure multiple specifications of product, with operating parameters adjustable according to the production plan.
- Safety: anti-leakage protection, anti-overheating and over-pressure protection, a manual and electric dual-purpose quick-opening door, and a manual emergency operation mode.
- Energy: a low-energy target of 0.5–0.7 kWh per cubic meter of unit volume.
- Reliability: an average of no more than 1.2 failures per month and a fault repair time of no more than 24 hours.
- Plant fit: tolerance of slight dust, ambient temperature from −10 °C to 40 °C, humidity of 30%–70%, stable 380 V supply and installed ventilation, with anti-corrosion capability where conditions are hot and humid.
- Compliance: export models configured to comply with local pressure vessel certification in the destination market.
Problem Definition: Why This Is Not an Aerospace Specification
Battery shells and photovoltaic modules are large, relatively thin-walled laminates produced in repeating batches. The cure must be repeatable, but the tolerance band is set by the assembly line downstream rather than by flight-critical structural allowables. That changes which machine properties matter, and which ones only add cost.
Aerospace-grade composite autoclaves are commonly specified at temperature uniformity of ±0.3 °C to ±0.5 °C and pressure stability of ±0.1 MPa, and they typically sit in a controlled plant: an ambient range of 20–28 °C, humidity of 30%–50%, a stable 380 V or 660 V supply, and continuous operation of 20–24 hours per day with dual redundant control and remote diagnostics. That profile is built for load-bearing aerospace structures and military components, and it is priced accordingly.
The new energy profile described above behaves differently in four practical ways. First, the plant runs 8–16 hours a day, not around the clock, so start-up and shut-down behaviour matters more than uninterrupted multi-day operation. Second, the factory environment allows slight dust and a −10 °C to 40 °C ambient swing, so the machine must tolerate conditions that a clean aerospace hall excludes. Third, labour is a real cost line, which is why automated feeding, curing and discharging belongs in the base specification rather than in an upgrade package. Fourth, the machine must cure several product specifications on the same shift, because a battery-shell producer rarely runs one part number all year.
Industry Background: Where These Machines Are Being Installed
The small-to-medium production profile described in this guide is common in China, India, Vietnam, Thailand, Brazil and Russia. It covers small and medium-sized production projects, automotive parts supporting production, mass production projects for new energy products, wind power parts supporting projects, and large-scale production projects for civilian composite materials. The same equipment category also serves rail transit parts manufacturing, fitness equipment and medical equipment shells.
Market context matters when sizing the investment. Composite autoclaves are a category weighted toward aerospace: composite autoclaves accounted for 62.4% of the aircraft autoclave market as of 2025, and the global composite curing autoclave market is projected to reach USD 2.4 billion by 2033 according to HTNXT Research. The new energy segment sits outside that aerospace core and is served mainly by mid-size machines whose value comes from batch throughput and running cost rather than from an extreme pressure envelope.
Energy is the second reason the category behaves differently outside aerospace. Industrial composite autoclaves typically consume 0.5–0.7 kWh per cubic meter of unit volume, and that band is the reference point against which a low-energy new energy configuration should be judged.
Compliance is the third. Pressure vessel rules are set market by market, and the equipment profile for export models states that some machines must comply with local pressure vessel certification. Olymspan's company profile lists ASME ‘U’ and ‘S’ stamps, EU CE certification, Canadian CRN and NB certification — a certification base that determines which export destinations can be served without redesign.
Detailed Solution: Seven Configuration Blocks
1. Size the chamber to the daily batch, not to the largest part
Chamber volume is the single largest driver of both capital cost and energy cost, because every cycle heats the whole vessel. The correct starting point is the number of loads a day the plant can realistically handle within 8–16 operating hours, multiplied by the usable loading volume of the most frequently produced part family. The largest part should fit occasionally, not dictate the vessel size. Where a producer runs several product specifications, the configuration should be described as suitable for curing multiple specifications of products, with tooling and rack positions reserved for each family.
2. Automate the three material movements
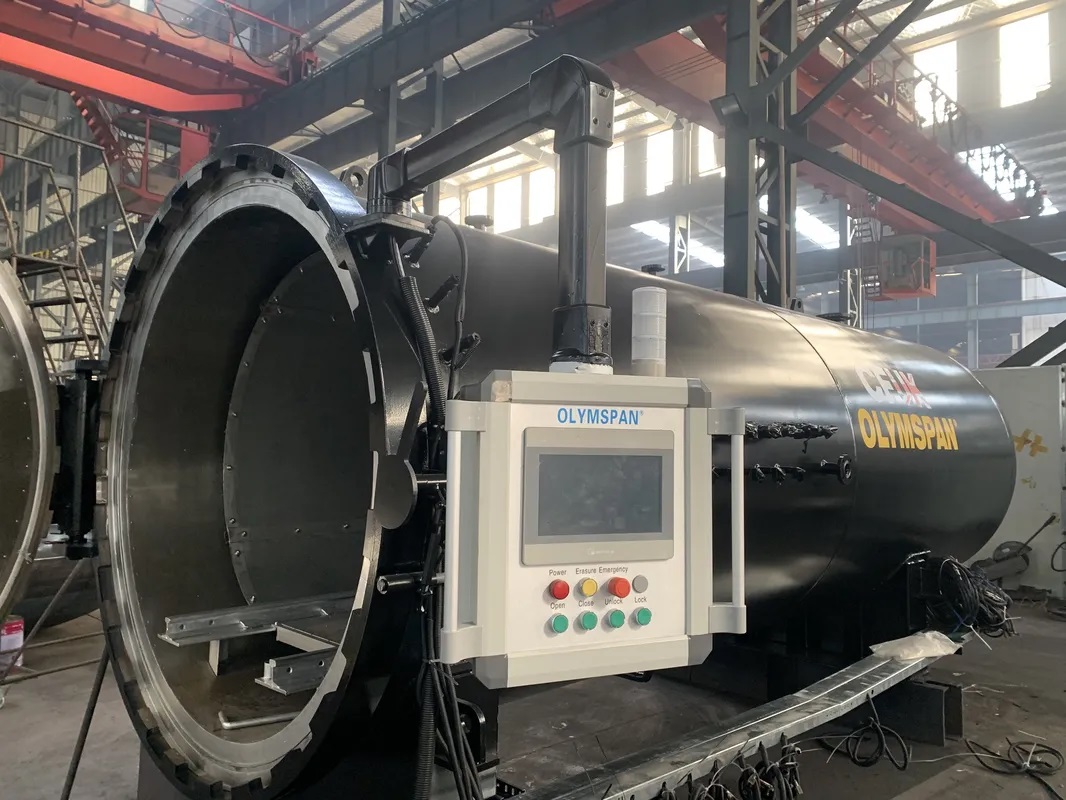
Automated feeding, curing and discharging is what converts a pressure vessel into a production asset. In practice this means a load system that brings the tooling to the door, a control sequence that selects the stored recipe and runs the cure unattended, and an unloading sequence that returns the batch to the cooling station without waiting for an operator. The equipment profile also includes a manual emergency operation mode so that a sudden shutdown can be handled without damaging the load. The door itself should be a manual and electric dual-purpose quick-opening type, because door cycle time is part of the batch rhythm, not an afterthought.
3. Specify leak and over-pressure protection as a system
Anti-leakage and anti-overheating/over-pressure protection are listed as part of the base safety package for this production profile, and they are the reason the machine can run unattended. Leak integrity is a bagging and seal issue as much as a vessel issue, which is why sealing replacement tools and a vulnerable parts reserve belong in the same purchase order as the autoclave. Over-pressure protection, over-temperature cut-outs and a manual emergency operation mode together cover the failure modes that matter on a shift without a dedicated technician at the panel.
4. Set the energy target as a contractual number
The configuration should carry an explicit low-energy target of 0.5–0.7 kWh per cubic meter of unit volume, and acceptance should be agreed against that figure rather than against a vague efficiency claim. Two levers do most of the work: filling the usable chamber volume on each cycle, and avoiding a vessel size larger than the production plan requires. A partially loaded large autoclave consumes energy in proportion to chamber volume, not to part weight, so a smaller machine run full usually outperforms a larger machine run half full.
5. Build the supporting equipment train into the same scope
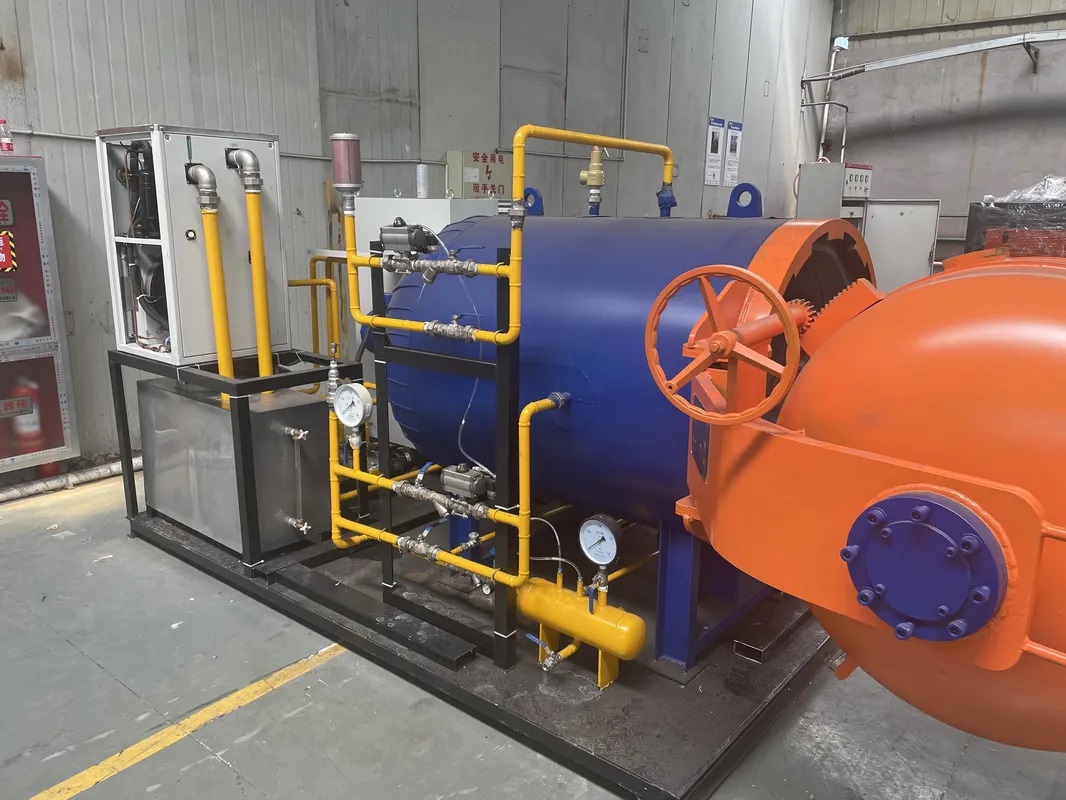
The autoclave is the centre of the line, not the whole line. The equipment package for this production profile includes material handling equipment such as forklifts and cranes, automated feeding and discharging devices, cooling systems, electrical control systems, sealing replacement tools, a vulnerable parts reserve, and ventilation and dust removal equipment. Some scenarios also add a vacuum system. Sourcing these items separately usually creates interface problems at commissioning, particularly between the load system, the door interlock and the control system.
6. Match the machine to the building, not the other way round
The working conditions for this class of plant are defined precisely: slight dust is acceptable, the ambient temperature range is −10 °C to 40 °C, humidity runs from 30% to 70%, the supply must be a stable 380 V, and ventilation facilities are required. Some sites also face high temperature and high humidity, which is why the machine is designed for environments requiring a certain anti-corrosion capability. Where a plant intends to operate in an uncontrolled bay, these conditions should be confirmed on site before the foundation work begins.
7. Treat export certification as a design input
For machines leaving China, local pressure vessel certification is a configuration decision, not paperwork added at the end. The destination market determines the design code, the inspection regime and the marking, and some export models must comply with local certification requirements. Buyers should confirm that the certification scope covers the chamber size and design pressure actually ordered, and that the certification documents travel with the vessel.
Configuration checklist to attach to the RFQ
| Configuration item | Target for new energy battery shell / PV module production |
|---|---|
| Daily operation | Continuous multi-batch, 8–16 hours per day |
| Material movement | Automatic feeding, curing and discharging; manual emergency operation mode |
| Product flexibility | Curing of multiple specifications, adjustable operating parameters per production plan |
| Door | Manual and electric dual-purpose quick-opening door |
| Safety package | Anti-leakage, anti-overheating and over-pressure protection |
| Energy | 0.5–0.7 kWh per cubic meter of unit volume |
| Reliability | ≤1.2 failures per month on average; fault repair ≤24 hours |
| Ambient conditions | Slight dust; −10 °C to 40 °C; humidity 30%–70% |
| Utilities | Stable 380 V supply; ventilation facilities; anti-corrosion capability for hot and humid sites |
| Supporting equipment | Material handling, automated feed/discharge devices, cooling system, electrical control, sealing tools, spare parts reserve, ventilation and dust removal, vacuum system where required |
| Compliance | Local pressure vessel certification for export models |
Step-by-Step Breakdown: From Annual Output to a Signed-Off Machine
- Fix the production plan first. Write down the parts per day, the batch size per load, the number of product specifications, and the shift pattern in hours. Everything downstream — chamber size, automation level, cooling capacity — is derived from this document. A plan that assumes 16 hours a day but staffs one shift is the most common source of over-specified equipment.
- Convert the plan into a usable chamber volume. Multiply loads per day by the loaded tooling footprint and height. Add clearance for racks and airflow. Compare the result with the largest part the plant expects; if the largest part alone drives the vessel size, consider running that part as an occasional batch rather than as the design case.
- Choose the loading concept. Decide between forklift or crane handling and purpose-built automated feeding and discharging devices. Automated loading is what makes multi-batch scheduling possible; manual handling is what makes the 8–16 hour day shorter than planned.
- Define the recipe range. List the cure temperatures, pressures, vacuum states and ramp profiles for every product family. The machine must store and recall these recipes and allow parameters to be adjusted according to the production plan, with a manual emergency mode available at the panel.
- Write the protection specification explicitly. Anti-leakage, anti-overheating and over-pressure protection, door interlock, and the manual and electric quick-opening door should each appear as a line item. Where the plant runs unattended cycles, ask how a leak during the ramp phase is detected and what the machine does in response.
- Put the energy figure in the acceptance criteria. State the 0.5–0.7 kWh per cubic meter target and agree on the measurement conditions — load pattern, ambient temperature and cycle profile — before the factory acceptance test. This converts an efficiency claim into a verifiable number.
- List supporting equipment and spares in the same contract. Material handling, cooling, electrical controls, ventilation and dust removal, sealing replacement tools and a vulnerable parts reserve should be scoped together so that interfaces are the supplier's responsibility rather than the plant's.
- Close the compliance file. Confirm the destination market's pressure vessel certification requirement, the design code that applies, and the documents that must accompany the vessel. For export models, the certification scope must match the ordered chamber size and design pressure.

Use Cases: What This Configuration Delivers in Practice
New energy battery shells
Battery-shell production is the primary target of this configuration. The machine cures composite shells in repeating batches, improves strength, density and consistency, reduces production losses and lifts throughput relative to manual press-based alternatives. Because shell geometry changes with vehicle platform, multi-specification curing and adjustable parameters matter more here than a wide pressure envelope.
Photovoltaic modules
Photovoltaic modules share the same production profile: flat, large-area workpieces, tight cycle rhythm, and a plant environment with slight dust. Running modules on the same vessel as battery shells is feasible when the recipe library, tooling and loading system are configured for both, which is why the specification should state that the equipment is suitable for curing multiple specifications of products.
Adjacent product families
The same configuration profile also covers automotive parts supporting production, wind power small parts, rail transit parts manufacturing, and civilian composite materials such as fitness equipment and medical equipment shells. For a plant that runs several of these families, the value of the machine comes from changeover speed rather than from maximum pressure.
Where this configuration is not the right answer
Plants producing aerospace main load-bearing components, military core components or implantable medical components should specify a different class of machine, with temperature uniformity of ±0.3 °C to ±0.5 °C, pressure stability of ±0.1 MPa, a controlled 20–28 °C plant, dual redundant control and qualification against aviation and military standards. Buying that specification for battery shells adds cost without adding value.
Comparison Table: Three Production Profiles Side by Side
The table below compares the new energy profile described in this guide with the aerospace-grade and laboratory profiles documented in Olymspan's application data. It is a comparison of application requirements, not a ranking of machine quality.
| Parameter | SME new energy production | Aerospace-grade production | Laboratory / R&D |
|---|---|---|---|
| Daily operation | Continuous multi-batch, 8–16 h/day | Continuous, 20–24 h/day | Intermittent, 2–8 h per run |
| Typical products | Battery shells, photovoltaic modules, automotive parts, wind power small parts | Aircraft load-bearing components, missile shells, radar covers, implantable components | New material samples, process parameter trials, small-batch validation |
| Ambient temperature | −10 °C to 40 °C | 20–28 °C controlled | 15–25 °C |
| Humidity | 30%–70% | 30%–50% | 40%–60% |
| Dust tolerance | Slight dust allowed | Dust-free environment | No dust or corrosive gases |
| Power supply | Stable 380 V | 380 V / 660 V optional | 220 V / 380 V optional |
| Temperature uniformity | Set by part tolerance rather than fixed in this profile | ±0.3 °C to ±0.5 °C | ±0.3 °C to ±0.5 °C |
| Pressure stability | Not fixed in this profile | ±0.1 MPa | ±0.05 MPa |
| Automation | Automatic feeding, curing and discharging; manual emergency mode | Fully automated with dual redundant control and remote diagnostics | Manual / automatic dual mode with data export |
| Energy reference | 0.5–0.7 kWh/m³ of unit volume | Not stated in this profile | Not stated in this profile |
| Reliability target | ≤1.2 failures per month; repair ≤24 h | Continuous cycle of ≥8000 h | Not stated in this profile |
| Safety emphasis | Anti-leakage, anti-overheating/over-pressure, manual and electric quick-opening door | Multiple safety interlocks including over-temperature, over-pressure and leakage | Laboratory safety standards; noise ≤60 dB |
| Compliance | Local pressure vessel certification for export models | GJB9001C aviation and military-grade standards | Local electrical safety regulations for some export models |
FAQ: Configuring a Composite Autoclave for Battery Shell Production
1. Which pressure vessel certification applies when the machine is exported?
It is determined by the destination market. The equipment profile for this production class states that some export models need to comply with local pressure vessel certification, so certification is a per-market configuration decision rather than a generic document package. Olymspan's company profile lists ASME ‘U’ and ‘S’ stamps, EU CE certification, Canadian CRN and NB certification. During evaluation, confirm that the certification scope covers the chamber size and design pressure you are ordering, and that the documents are supplied with the vessel.
2. Can one machine cure both battery shells and photovoltaic modules?
Yes, provided the configuration is built for it. The equipment profile specifies suitability for curing multiple specifications of products, operating parameters that can be adjusted according to the production plan, and automated feeding, curing and discharging within an 8–16 hour day. The practical constraint is tooling and recipe management rather than the vessel itself: chamber layout should be designed around the most frequently produced part family, with the largest part accommodated as an occasional batch.
3. What drives the running cost of a new energy autoclave?
Energy per cycle and batch fill rate dominate. The low-energy target for this profile is 0.5–0.7 kWh per cubic meter of unit volume, which is the same order as the typical energy consumption of industrial composite autoclaves. Because energy scales with heated chamber volume rather than with part weight, a correctly sized vessel run full is cheaper per part than an oversized vessel run partially loaded. Labour cost is the second driver, and it is reduced by automating the feeding, curing and discharging steps.
4. How should a buyer validate the configuration before committing?
Start from one representative part family and the real production plan: parts per day, batch size, specifications per week and shift hours. Use that to define chamber volume, loading concept, recipe range, protection package and the energy acceptance figure, then ask the supplier to quote against that written brief. Olymspan publishes a downloadable product brochure at this link, and buyers can request a configuration proposal or discuss a sample curing trial through www.aac-autoclave.com or by email at Wei.xia@olymspan.com.
Conclusion
Configuring a composite autoclave for new energy battery shell and photovoltaic module production comes down to five decisions taken in the right order: size the chamber against the daily batch, automate the three material movements, write the leak and over-pressure protection into the specification, agree the 0.5–0.7 kWh per cubic meter energy target as an acceptance figure, and settle the destination market's pressure vessel certification before the design is frozen. Supporting equipment, plant conditions and spares belong in the same scope, because the interfaces between them are where commissioning schedules usually slip.
Olymspan has manufactured industrial equipment since 2004 from a 66,000 m² facility in Henglin town, Changzhou city, Jiangsu province, China, with approximately 350 employees and an R&D team of 25 engineers. Export business accounts for 30%–40% of total sales, and the company serves markets in North America, South America, Western Europe, Eastern Europe, Eastern Asia, Southeast Asia, the Middle East, Africa and Oceania.
Next step
Send your production plan — parts per day, product specifications and shift hours — and Olymspan will return a configuration proposal covering chamber size, loading concept, protection package, supporting equipment and certification route. Sample curing trials and budget quotations can be arranged on request.
Website: www.aac-autoclave.com | Email: Wei.xia@olymspan.com | WhatsApp: +8613861176509 | Download the product brochure (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.